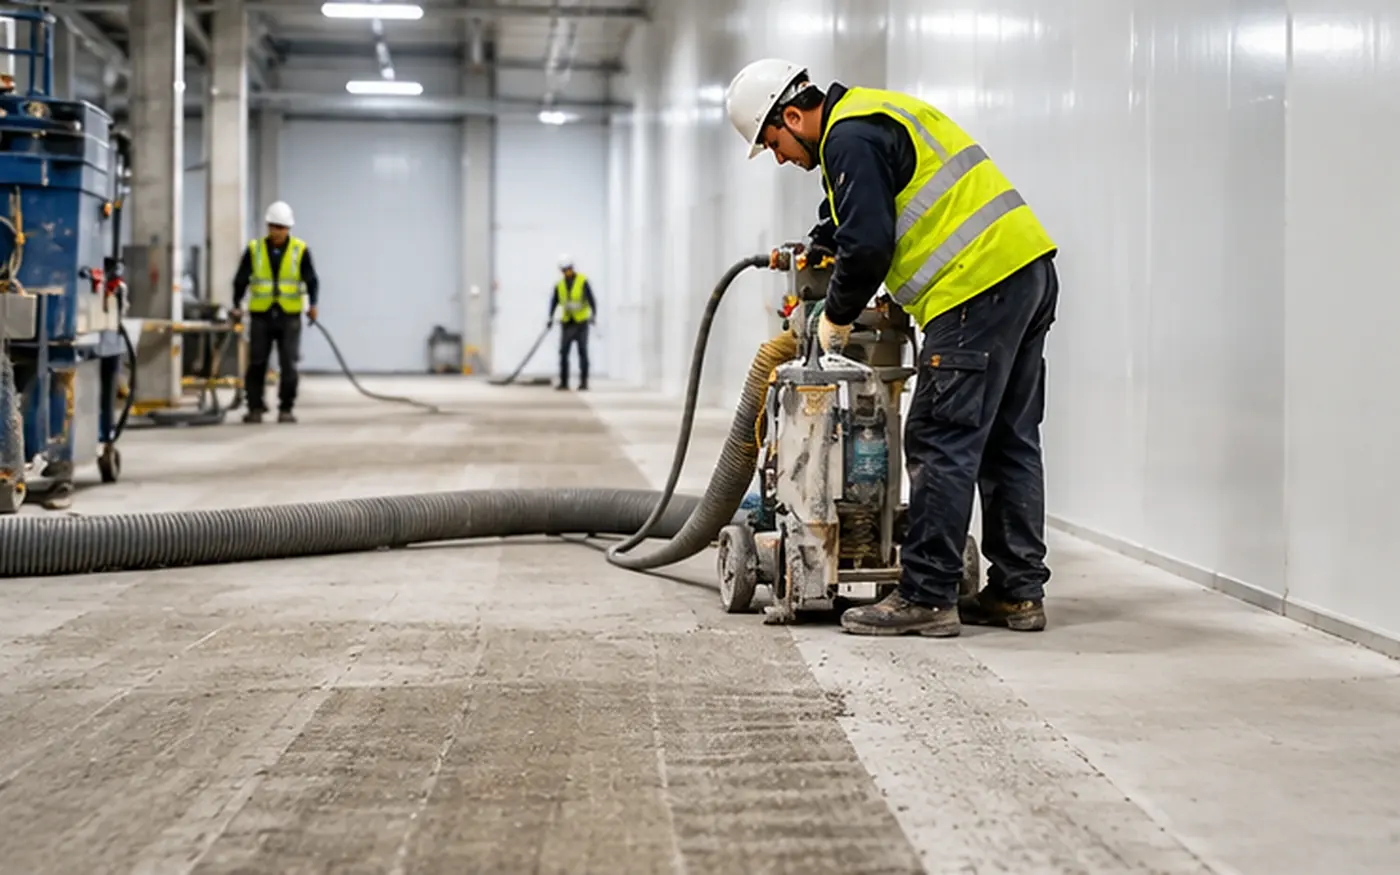
Substrate Preparation
Shot-blasting and grinding the concrete to a sound, open profile — the mechanical key every heavy-duty resin floor depends on.
PreparationSome environments destroy ordinary floors. Commercial kitchens flood their floors with boiling water and grease. Dairies and beverage plants subject them to constant wet processing and aggressive cleaning. Cold stores freeze them solid, then thaw them. Chemical and pharmaceutical plants expose them to acids and solvents. In these conditions, a standard epoxy floor cracks, softens, delaminates, or degrades — and a failed floor means downtime, contamination risk, and expensive re-work. Ucrete exists precisely for these environments.
Ucrete is a heavy-duty polyurethane resin flooring system from Sika — the specified choice for the world's most demanding industrial and food-production facilities. Its dense, seamless, impact-resistant surface withstands thermal shock from steam cleaning and hot spills, remains tough at cold-store temperatures, resists a broad range of aggressive chemicals, and carries heavy mechanical and traffic loads year after year. It is not a decorative floor — it is an engineered working surface built to keep a facility running.
Hill Technical Services is a certified Ucrete applicator. With a premium resin system, the installation matters as much as the product: correct substrate preparation, priming, mixing, and trowel or screed application are what turn a high-performance material into a floor that lasts. Our trained crews apply each system to the manufacturer's protocol, install integral hygienic coving where required, and plan every project around your production schedule to minimise downtime. The result is a seamless, cleanable, HACCP-friendly floor engineered for long, hard service.
Shot-blasting and grinding the concrete to a sound, open profile — the mechanical key every heavy-duty resin floor depends on.
Preparation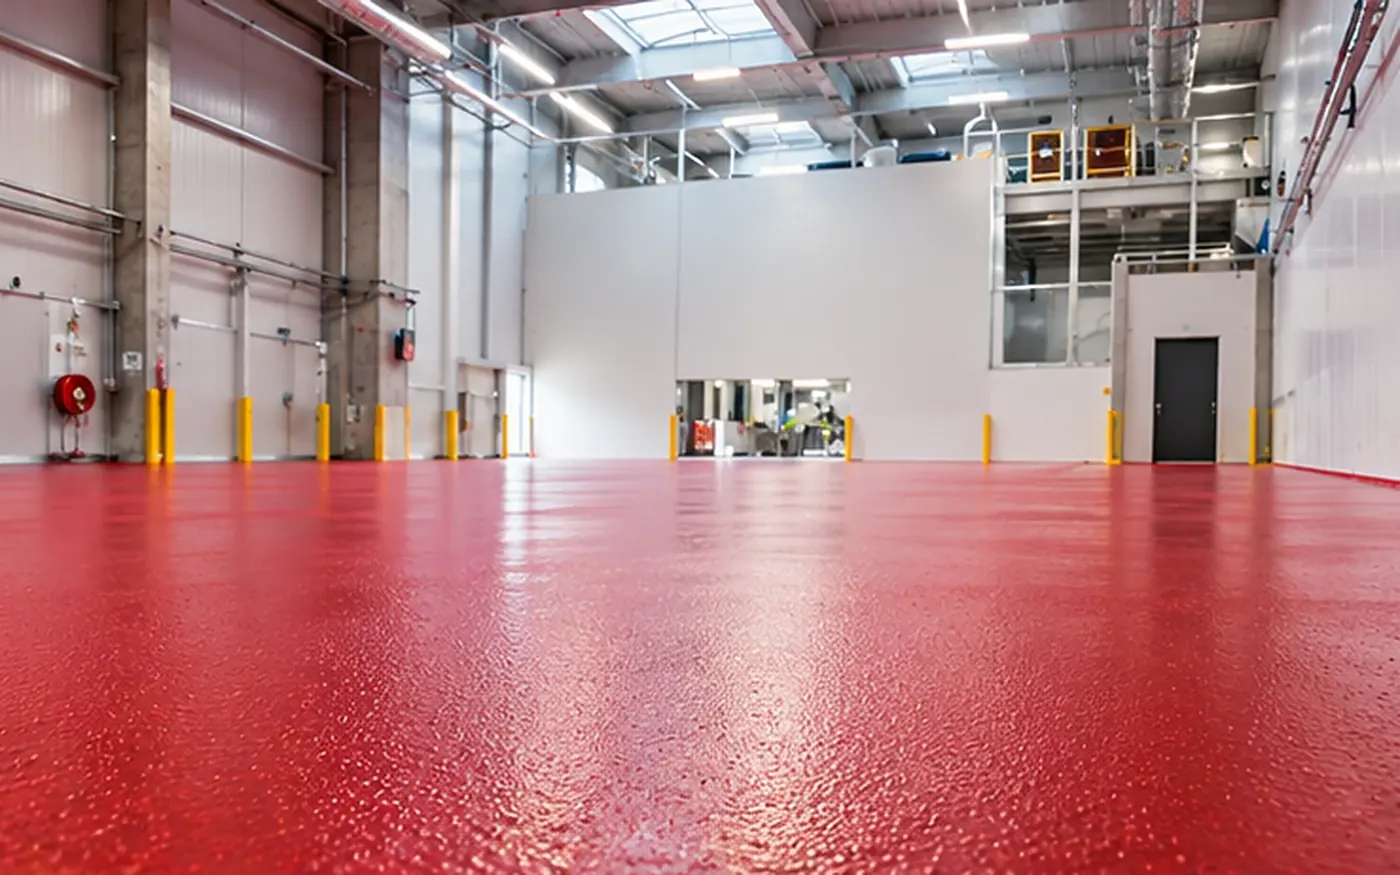
A seamless, high-gloss Ucrete floor finished for continuous heavy traffic, impact, and aggressive cleaning.
Industrial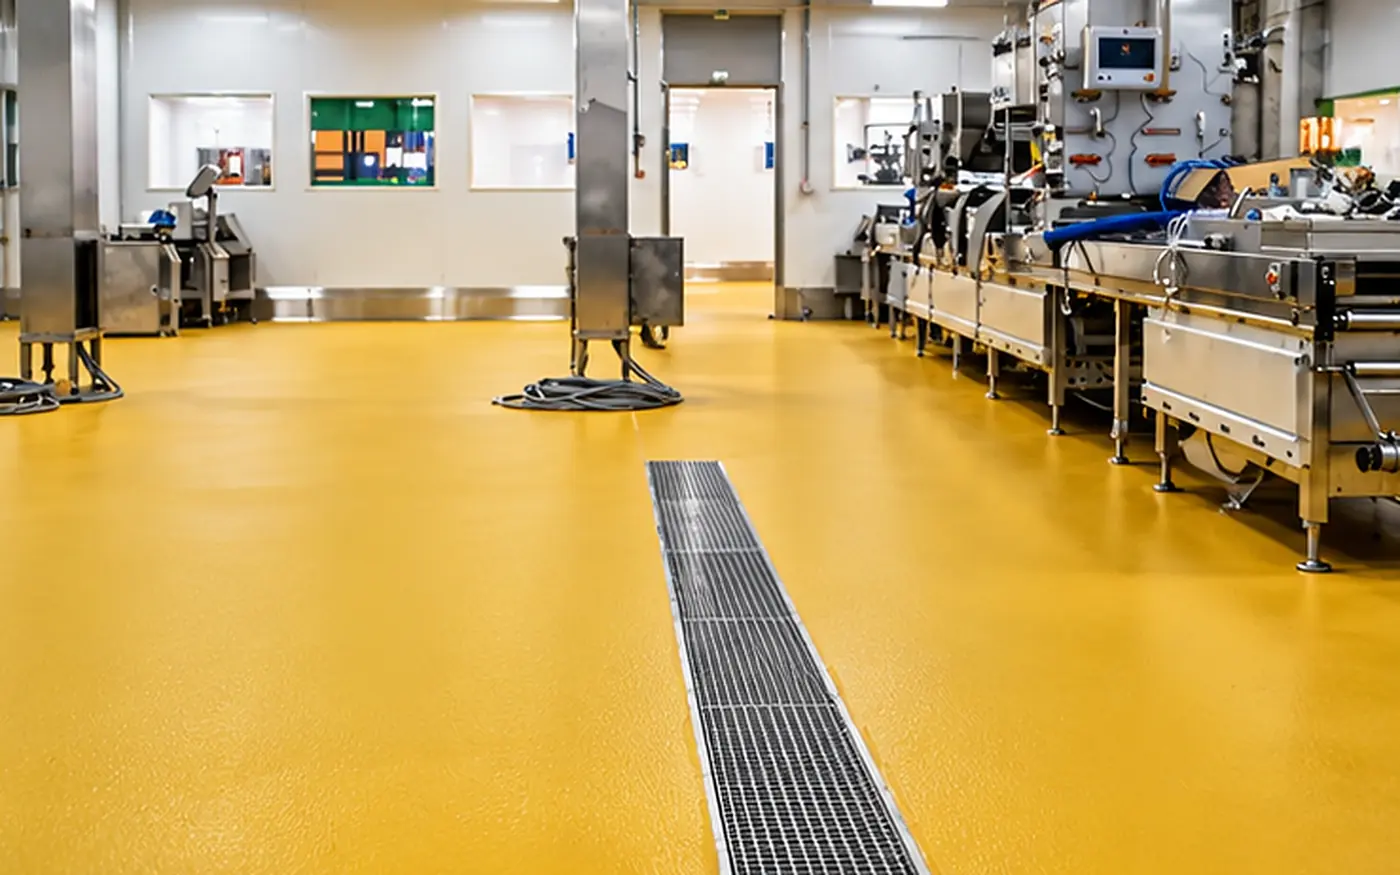
Hygienic Ucrete flooring with integrated drainage falls for a wet-process food production line.
Food ProcessingThe heavy-duty industrial workhorse — a dense, trowel-applied polyurethane floor for the most aggressive mechanical, thermal, and chemical conditions. Built for uncompromising performance in continuous heavy-traffic operations.
A high-build, thick-section system engineered for the toughest thermal-shock and heavy-load environments. UD200 tolerates repeated steam cleaning and boiling-water exposure while carrying intense mechanical loading.
Medium-duty (MF) and industrial (IF) self-smoothing finishes that deliver a smoother, more decorative surface while retaining Ucrete's chemical and hygiene performance — ideal where appearance and cleanability both matter.
Seamless, radiused coving formed at wall and plinth junctions to eliminate the dirt-trapping right-angle corners that open floors leave behind. Essential for hygienic, washdown-friendly food and pharma environments.
Regulating and levelling screeds that restore and true up damaged or uneven substrates before the finish system is applied — ensuring the final floor has a sound, level base to perform on.
Engineered anti-slip textures and integrated drainage detailing specified to the wet or greasy conditions of your process — keeping the floor safe underfoot while managing liquids to falls and channels.
We shot-blast or grind the concrete to a sound, open profile, cut in anchor grooves at edges and drains, and repair defects — the mechanical key that a heavy-duty resin floor depends on for lifelong adhesion.
We match the Ucrete grade, thickness, texture, and coving to your process — temperature range, chemical exposure, loading, and hygiene requirements — and confirm it against your production schedule.
As approved applicators, our crews prime, mix, and trowel or screed each layer to the manufacturer's protocol, forming integral coving and detailing drainage falls as specified.
We manage cure and rapid return to service to minimise your downtime, then hand over with datasheets, maintenance guidance, and warranty documentation for a certified installation.
Ucrete is a heavy-duty polyurethane (PU) resin flooring system, now a Sika brand, engineered for the toughest industrial and food-processing environments in the world. It is a dense, seamless, and impact-resistant floor that withstands aggressive chemicals, heavy mechanical loading, and extreme temperature swings — from cold-store freezing to boiling-water and steam cleaning. Where a standard epoxy floor would crack, delaminate, or degrade, a Ucrete floor keeps performing, which is why it is specified for food, beverage, pharmaceutical, and chemical facilities globally.
Standard epoxy floors are excellent for many environments, but they have limits: they can soften and fail under thermal shock, become brittle in freezing conditions, and be attacked by certain acids and organic solvents. Ucrete's polyurethane chemistry is far more resilient. It resists thermal shock from steam cleaning and hot-liquid spills, remains tough in cold stores down to very low temperatures, and stands up to a much broader range of aggressive chemicals. For heavy-duty, hygiene-critical, or temperature-extreme areas, Ucrete delivers a longer service life and lower lifetime cost than epoxy — which is exactly why it is a premium, specified system.
Yes — thermal-shock resistance is one of Ucrete's defining strengths. The heavy-duty grades are designed to tolerate repeated exposure to boiling water, hot-liquid spills, and high-temperature steam or jet washing without cracking, blistering, or debonding from the substrate. This makes Ucrete the natural choice for commercial kitchens, dairies, beverage plants, and any wet-process area where floors are cleaned aggressively and frequently. The exact grade and thickness are specified to match the temperature conditions of your process.
Ucrete is widely used in food and beverage manufacturing precisely because it supports hygienic, HACCP-based operations. The floor is seamless, dense, and non-porous, so it does not harbour bacteria and is easy to clean and disinfect. It can be installed with integral coving at wall junctions to eliminate the dirt-trapping corners that open floors leave behind, and many Ucrete systems carry certifications for use in food-production environments. Installed correctly, it forms a durable, cleanable, and taint-free surface suited to the most demanding hygiene regimes.
Installation time depends on the area, the system selected, and the amount of substrate preparation and coving required, but a key advantage of Ucrete is its rapid return to service. Many systems cure quickly enough to allow foot traffic and return to operation within a short window, which minimises costly downtime for working facilities. Hill plans each project around your production schedule — including phased or out-of-hours working where needed — and confirms the exact preparation, application, and cure timeline as part of the specification.
Yes. Hill Technical Services is an approved applicator for Sika Ucrete systems. Our crews are trained in the correct substrate preparation, priming, mixing, and trowel or screed application that these high-performance floors demand — because with a premium resin system, the quality of the installation is as important as the product itself. We apply the specified system to the manufacturer's protocol and provide the documentation and warranty support that come with a certified installation.